Technology for Grinding, especially Jig Grinding
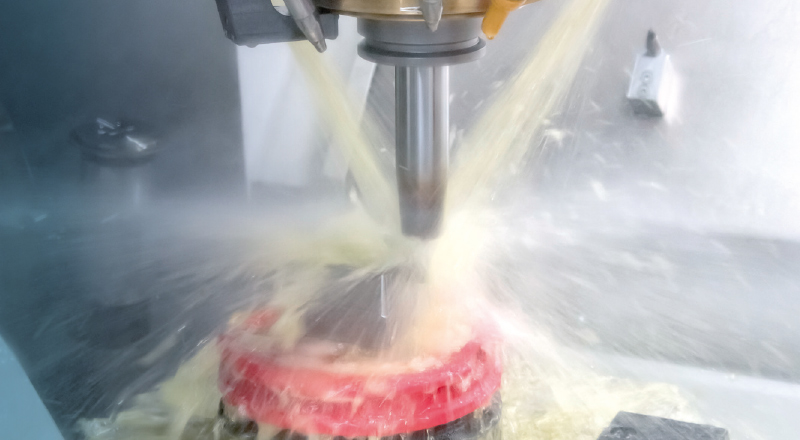
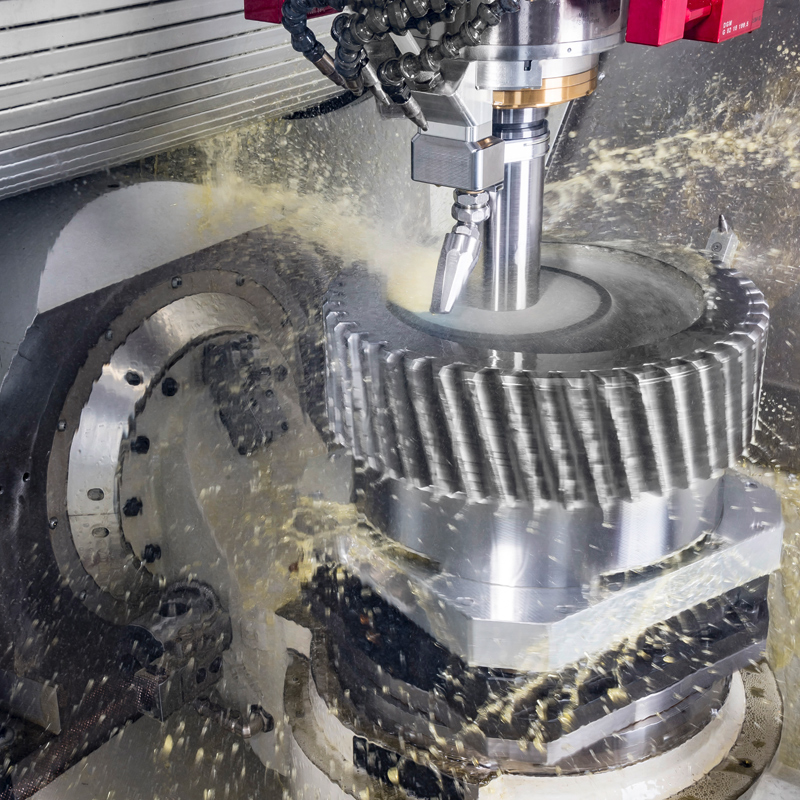
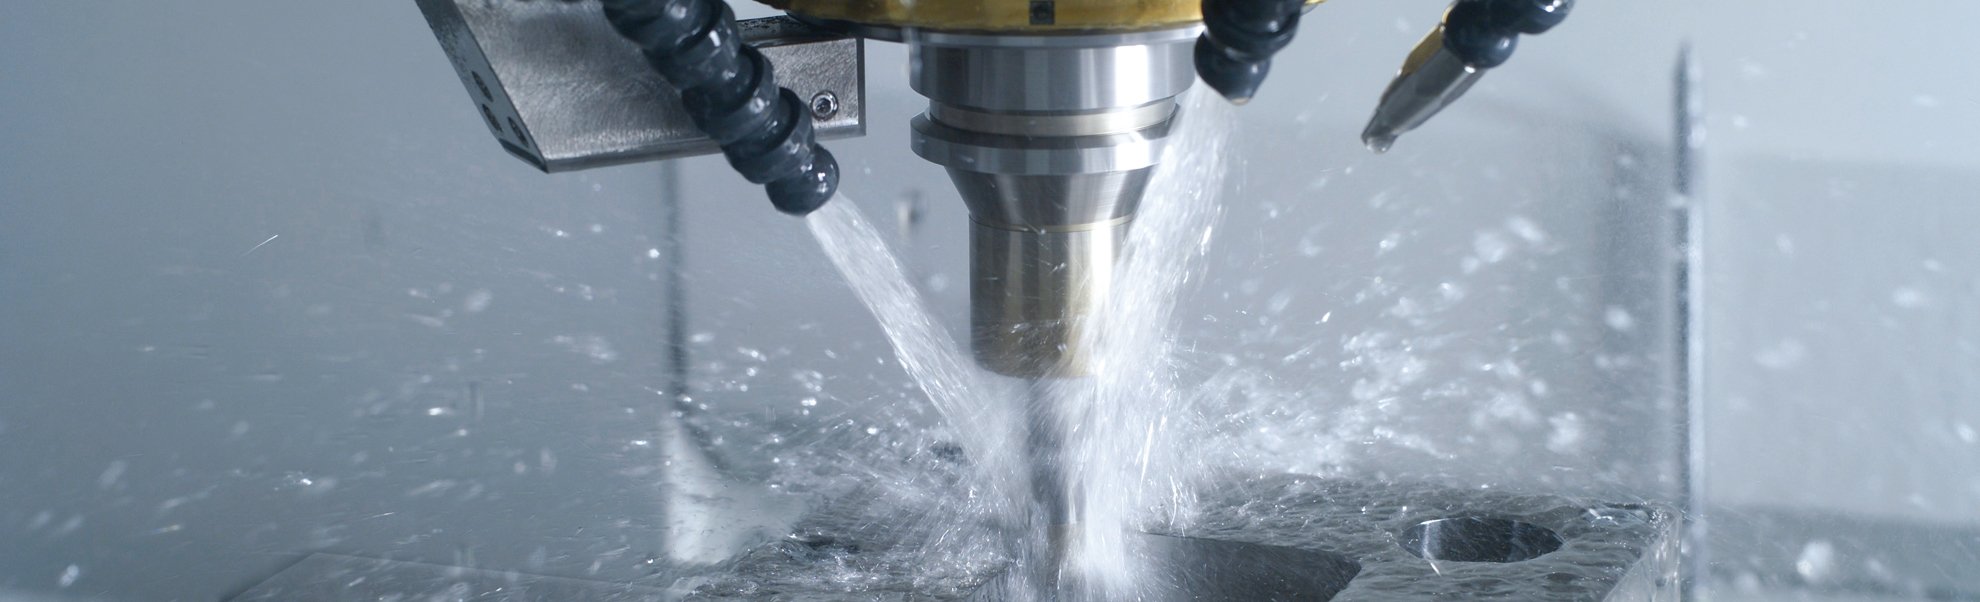
Combining milling and grinding, especially jig grinding in a single set-up can lead to a significant increase in efficiency in many applications. Roughing is carried out by milling, whilst high precision sometimes in sub-micrometre range is achieved through grinding, mostly jig grinding. Milled 3D contours fit perfectly with ground areas, etc. All machines except the RXP400 can be fully equipped for grinding.
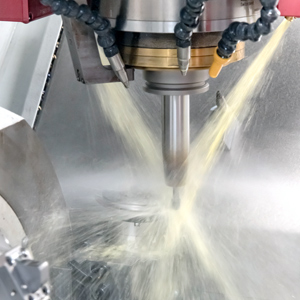
There are two strategies available for grinding: fast stroke chop grinding, familiar from jig grinding machines, and slow stroke chop grinding with a higher feed rate and multiple passes, which puts less dynamic stress on the machine structure and therefore results in even higher accuracies. Flushing oil lubrication is the preferred lubrication, with the oil precisely temperature-controlled. Surface finishes are in the nanometre range, well below 0.01 µm.
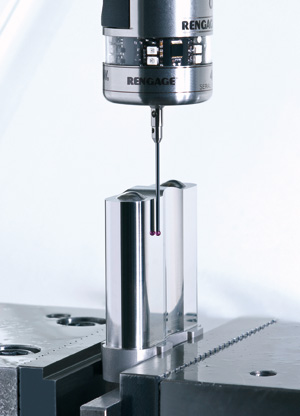
Where highest precision requirements in sub-micrometre range apply, the workpiece firstly is finished-ground with a small allowance, then the dimensions achieved are measured using the 3D touch probe, the final infeed is automatically calculated by the RMS6 control system, and finally the workpiece is finished-ground to the exact final dimensions. No operator intervention is required. This approach has proved particularly effective in jig grinding applications, but can also be used for machining tasks involving larger grinding tools.
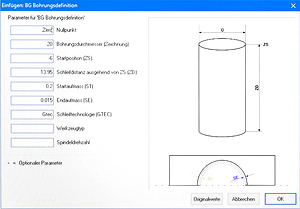
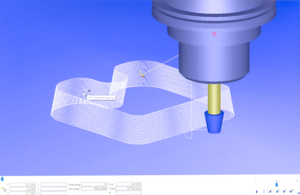
The RMS6 control differs significantly from other NC-controls in that it offers a very straightforward way for the programming of grinding operations directly at the control, as well as a comprehensive range of grinding cycles. In addition, geometries designed externally can be imported directly into the RMS6 control. 3- or 5‑axis machining of conical workpieces, including the necessary dressing of the grinding wheels, can also be programmed quickly.
Various cycles are available for the dressing of the grinding wheels. By carrying out a preliminary measurement using the measuring laser, the time needed to contact the dressing wheel with the grinding wheel can be reduced significantly.
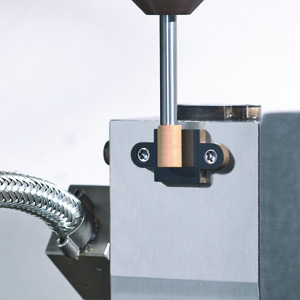
The sound detection-based measurement is used for
- precisely measuring the grinding wheel on diamond surfaces
- detecting the surface of the workpiece
- monitoring and optimizing the grinding process
- monitoring the dressing process
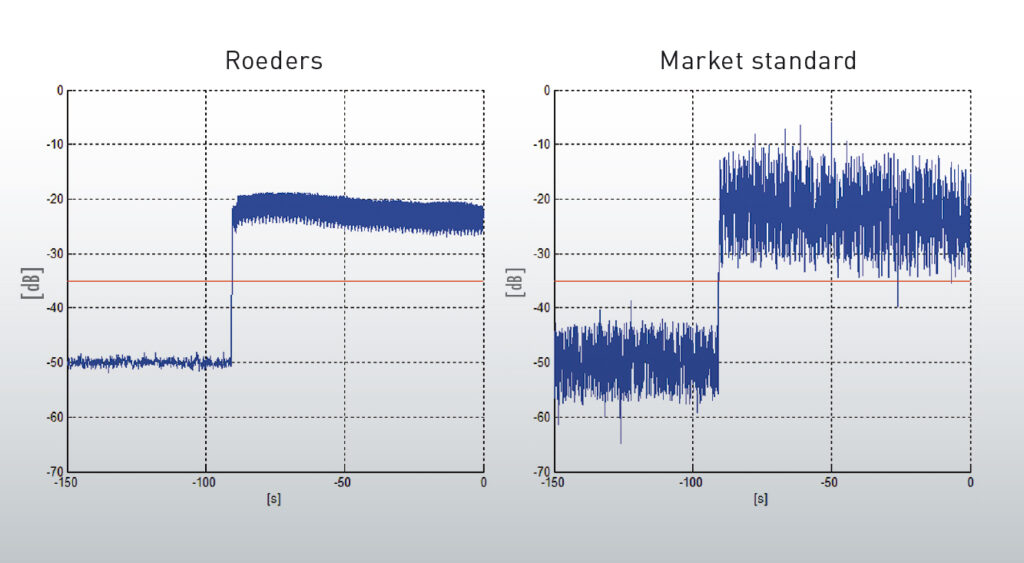
Using a proprietary development, Roeders has significantly improved the analysis of the sound signal, thereby substantially increasing precision and reliability. The visualization and parameterization of the signals are fully integrated into the RMS6 control.
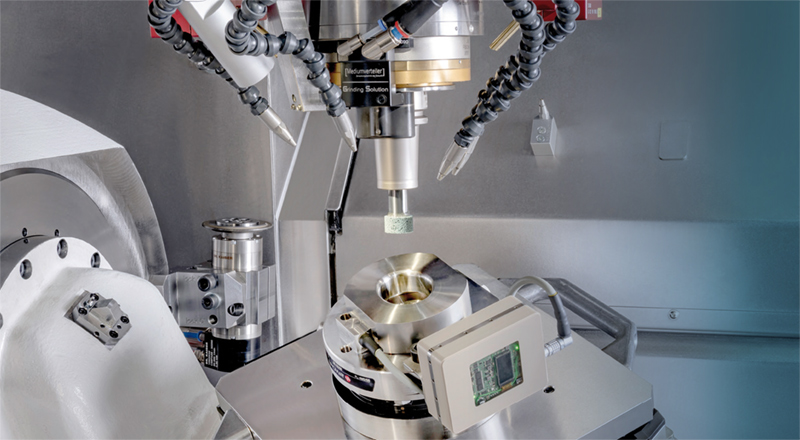
Thanks to a highly compact, wireless sound detection sensor – the result of many years of development – it is possible to carry out sound detection-based measurements on 5‑axis machines with outstanding signal quality and without the need for interfering cables. The results are in the sub-micrometre range. The sensor is activated automatically and switches to power-saving mode once machining is terminated complete. This makes it ideal for use in automated machines.
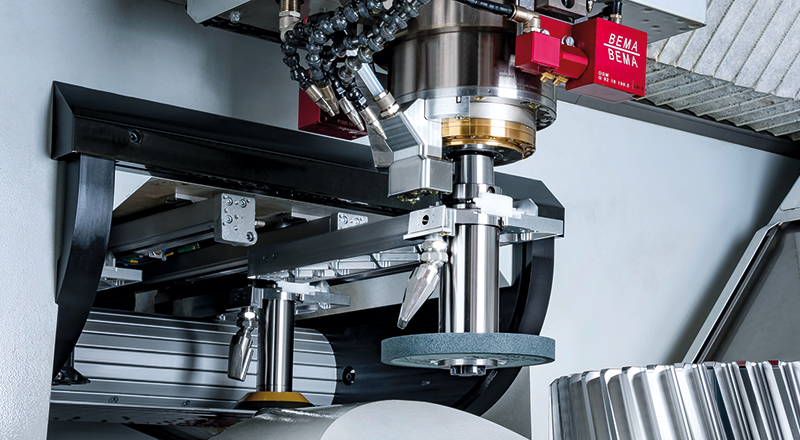
Large grinding wheels can be changed into the spindle automatically from an extra tool changer for large diameter tools.
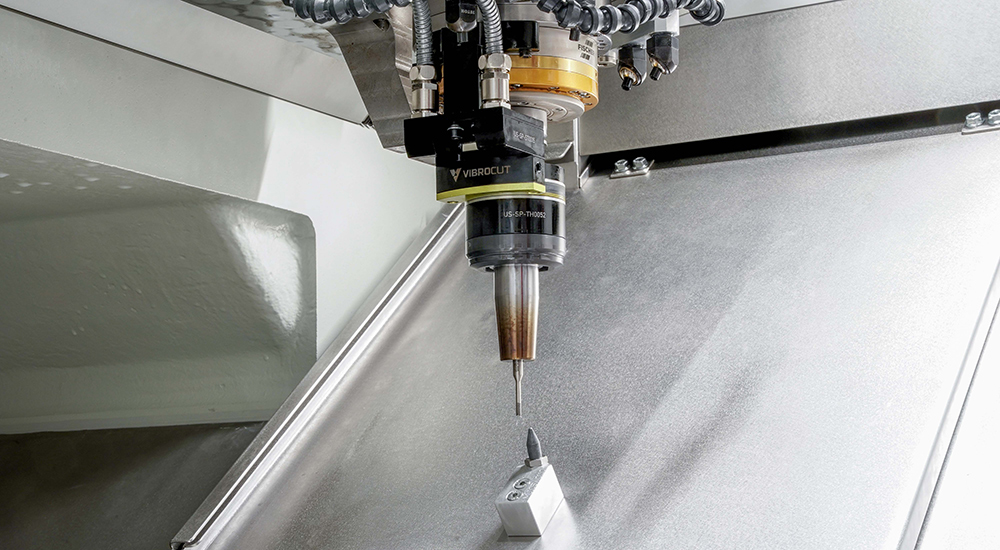
For machining brittle-hard materials such as glass or ceramics, a system for axial ultrasonic excitation of the tool is available, which may be fully integrated into the machine. The ultrasonic excitation takes place directly at the tool holder, so that the spindle is not affected by the excitation and is still available for machining without ultrasound. Ultrasound can significantly reduce the machining forces and thus in some applications the surface damage to the workpiece caused by machining. In some cases, higher machining feeds and removal rates are possible.
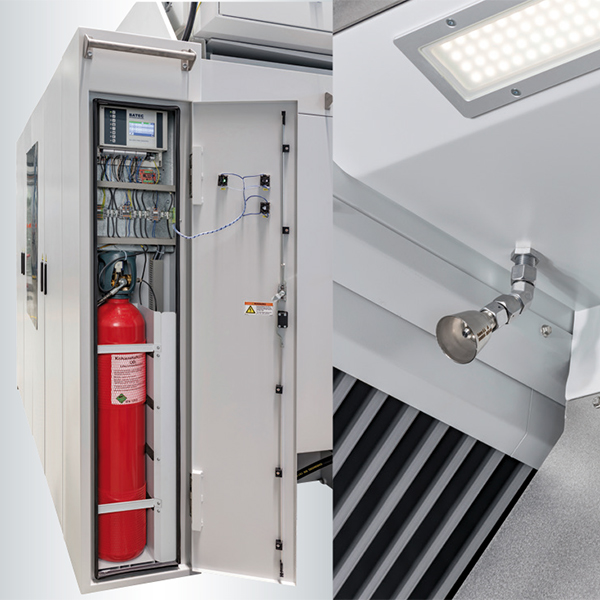
The best grinding results are achieved using fine-filtered, precisely temperature-controlled grinding oil. A CO₂ extinguishing system is available, or, particularly for workshops with limited space, an aerosol-based extinguishing system.