The Roeders Control RMS6
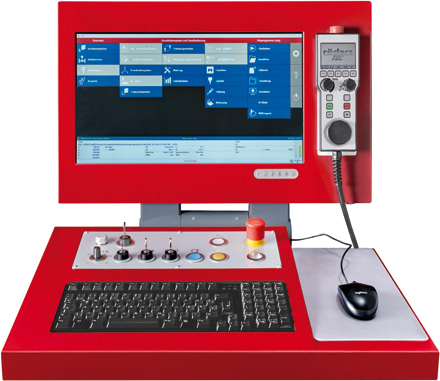
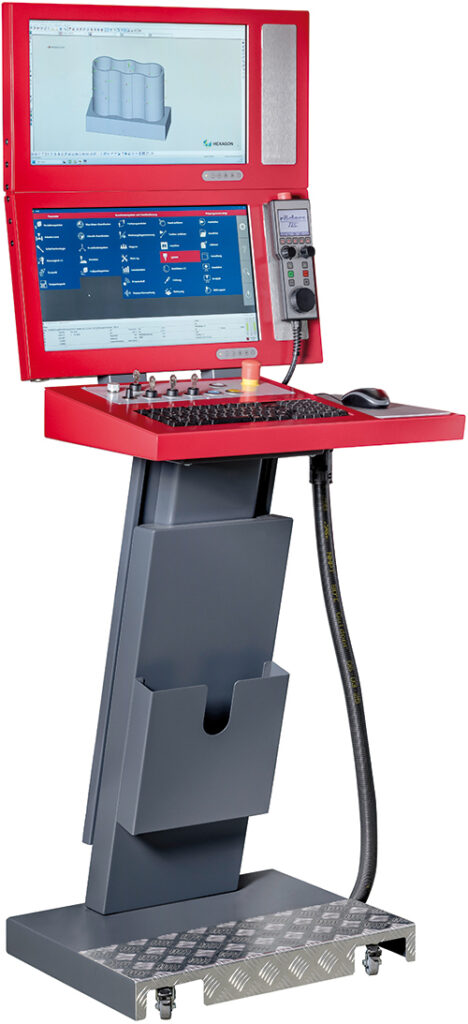
The Roeders RMS6 machine control system has been continuously developed and improved since 1994 to meet the most demanding requirements for precision and surface quality in milling and grinding. The open and robust control system is based on two PC-based industrial computers. A 21,5” TFT screen is standard. The few control elements are arranged in a very clear and logical manner. Running on Microsoft Windows, the user interface is easy to operate and requires only a very short training period. Numerous features, some of which are patented, have been integrated into the RMS6 specifically for milling and grinding. Post-processors for standard CAM systems are available. The RMS6 processes Heidenhain® and ISO program code.
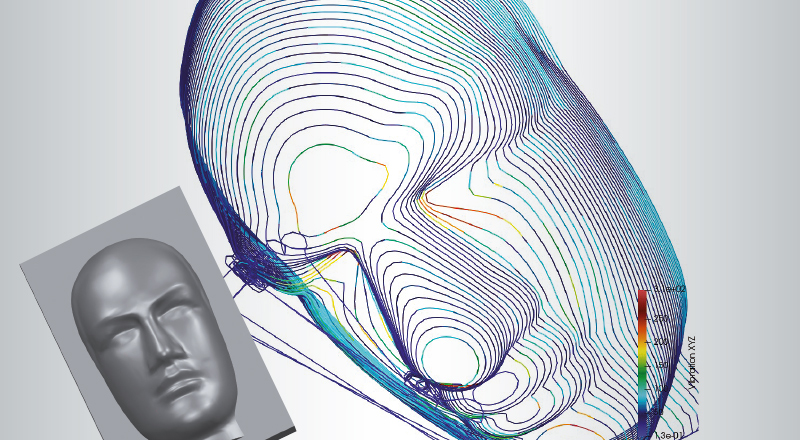
Vibration monitoring of the spindle
The use of high-speed spindles requires a limitation of the maximum spindle load in order to avoid bearing damage or a severe reduction in service life. Optionally, the spindles can be equipped with vibration sensors. A function in the control can be activated that automatically reduces the feed and, if necessary, the RPM of the spindle in the event of high vibrations. In addition, a coloured graphic illustration of the vibrations along the milling path is possible. As a result, any areas in the milling path with high vibrations can easily be identified and can safely be avoided in recurring machining processes by adapting the CAM programming.
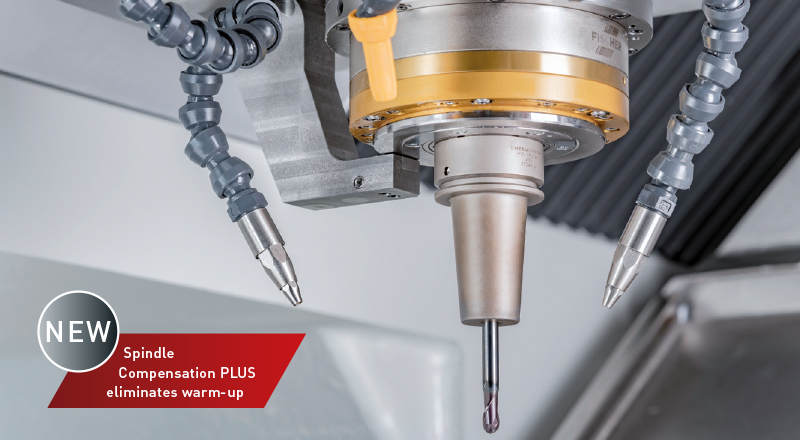
Compensation of spindle elongation
Roeders machines have been known for years for their external high-precision sensor for compensating the spindle elongation . A holder fixed in the casting of the Z‑axis and kept geometrically stable with a temperature-controlled circuit carries a sensor at the end that contactless measures the displacement of the rotating spindle shaft in nanometre range. This is compensated for in the control system. Since the heat from the spindle shaft is transferred into the tool holder and it also lengthens as a result, a short warm-up phase had to be programmed for high-precision machining applications before starting the machining operation.
Meanwhile, the Roeders technicians have succeeded in modelling the dynamic heating process directly after the spindle has accelerated to full RPM, so that with the new option Spindle Compensation PLUS a warm-up phase can be skipped completely in many applications.
Roeders is partner of the umati initiative of the German machine tool association VDW (umati = universal machine tool interface). The umati interface enables a standardised data transfer with the machines of numerous suppliers. umati is an essential step towards industry 4.0.
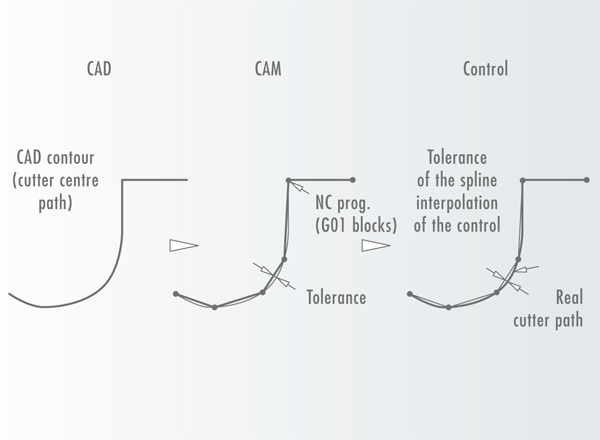
The development of the RMS6 focuses on an optimised machine control during the production of free-form surfaces and complex contours. The RMS6’s performance is correspondingly outstanding, with block processing times of less than 0.1 milliseconds and a lookahead of over 10,000 blocks. The spline interpolation along the toolpath specified by the CAM system is continuously refined down to the nanometre range. A smooth and harmonious toolpath ensures optimum machine behaviour.
All Roeders machines supplied since 1995 can cost-effectively be upgraded to the latest RMS6 control version due to the PC-based control hardware. This also makes older machines more precise and faster in their machining operations. Furthermore, the full range of newest RMS6 functions is available. If a customer uses several Roeders machines built in different years, it is easily possible to operate all machines with the latest – and therefore identical – RMS6 version.
A dual-screen option is available for the RMS6, for example, if the operator wishes to have the editor, design views of the workpiece or drawings open alongside the control system’s menu structure and status window.
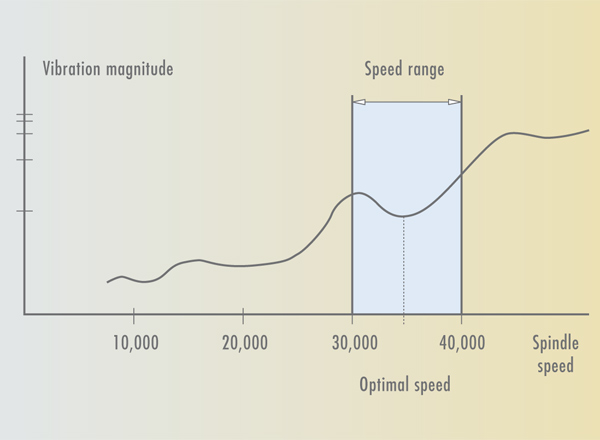
The vibrations of the main spindle do not necessarily increase steadily as the rpm rise. Depending on resonances, there are ranges with higher and lower vibration levels. For the machining process, exact rpm usually are not essential. With the automatic vibration optimisation, the RMS6 selects, within an rpm range specified by the operator, the rpm at which the spindle with the toolholder and tool clamped has the lowest level of vibration.
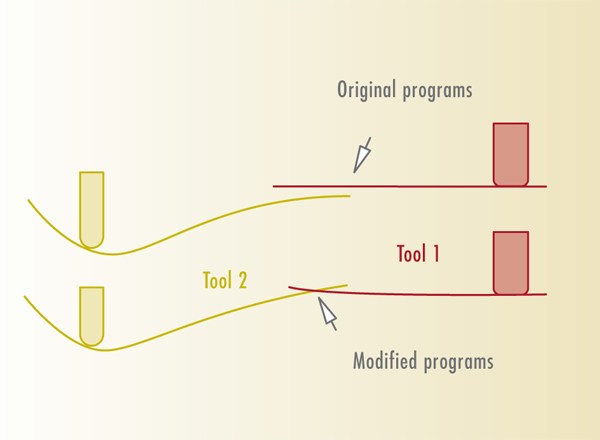
To avoid steps in transition areas that are machined using different tools, the RMS6 allows a setting to be specified whereby the edges of the machining areas are raised in such a way that a tangential transition is created between areas machined with different tools.
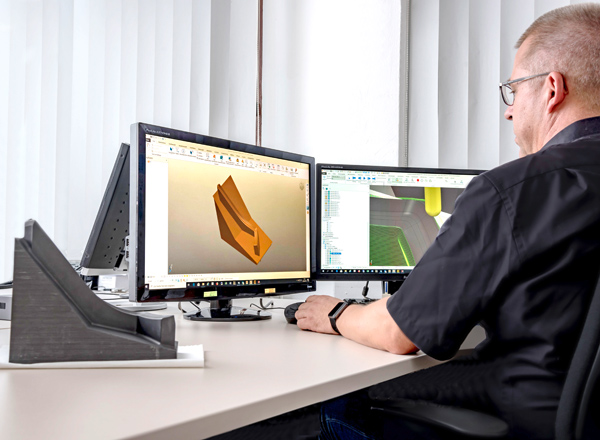
Post-processors are available for all leading CAM systems. A detailed post-processor manual is provided to optimise the interface between the RMS6 and the CAM system. In particular, for automated machine operation, machining programs can be generated reliably within the CAM system without the need for manual parameter input.
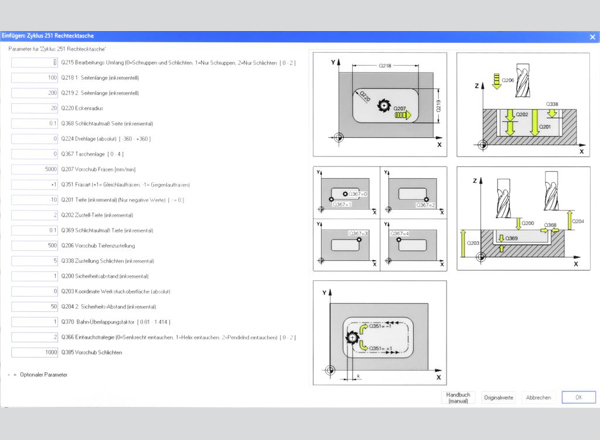
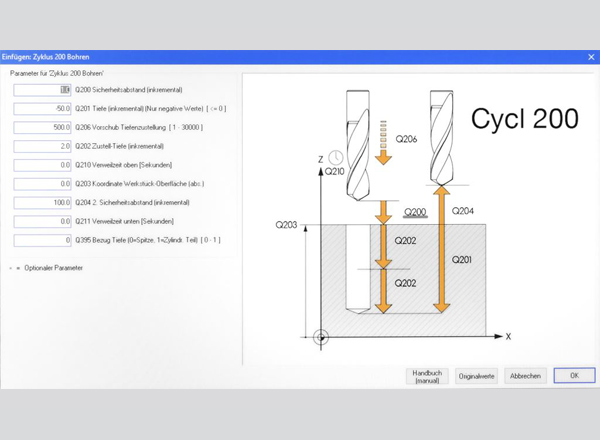
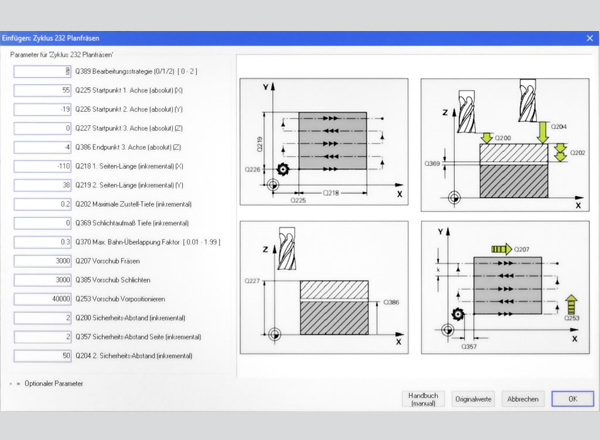
The RMS6 offers a high degree of flexibility when processing NC-programs for machining a workpiece. ISO (G‑code) and Heidenhain® NC-programs are possible and can also be used in combination. In addition, there is a considerable range of additional commands, extending standard NC-code as far as Basic-like programming, which opens up a wide range of possibilities, particularly for automation in specialised applications. Further commands can be added at customer’s request.
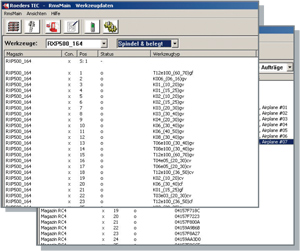
There are numerous strategies for the optimal use of tools, depending on the application. These relate to wear criteria, tool life and sister tools as well as measurement strategies, geometry recognition and inspection. To avoid the time-consuming task of entering tool data manually, a tool database is available, as is the option to import tool data and types.
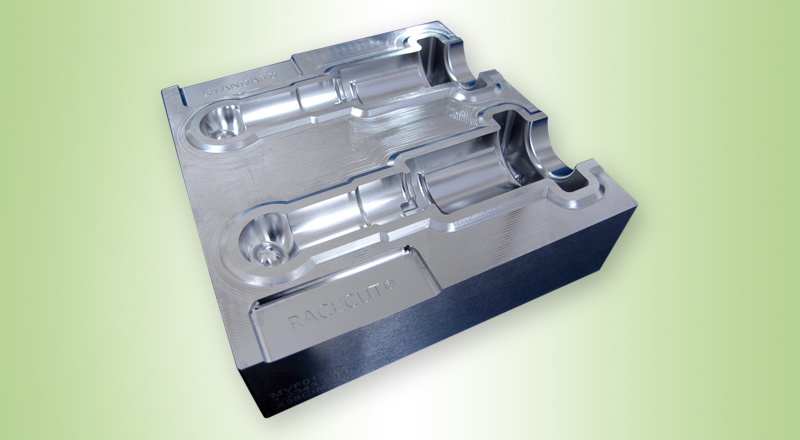
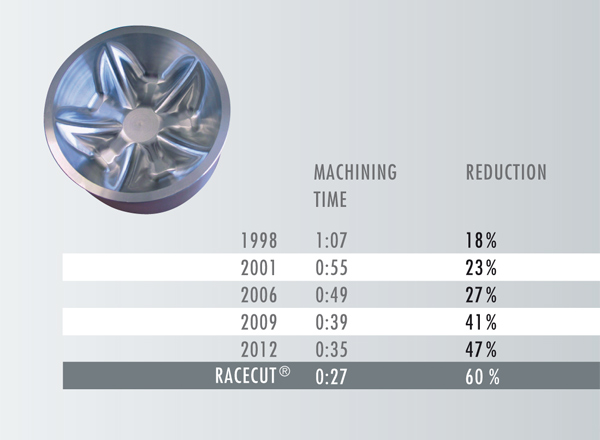
With RACECUT®, Roeders has once again achieved a performance boost for machining. This functionality in the RMS6 drastically reduces machining times by up to 20 per cent without compromising quality. It is based on further improvements for tool path planning within the control system and a drives control system operating at a frequency of 32 kHz. As the machine’s energy consumption remains relatively constant regardless of the selected dynamic settings, the energy savings are of a similar magnitude.
#Heidenhain is the registered trade mark of the Dr. Johannes Heidenhain GmbH.